Tube laser capacity: diameter is not the number that stops the job
Buyers specify a tube laser on diameter. The number that actually decides which machine they need is the weight of the tube, and the same 150 mm section can weigh 107 kg or 254 kg on a six metre stick.
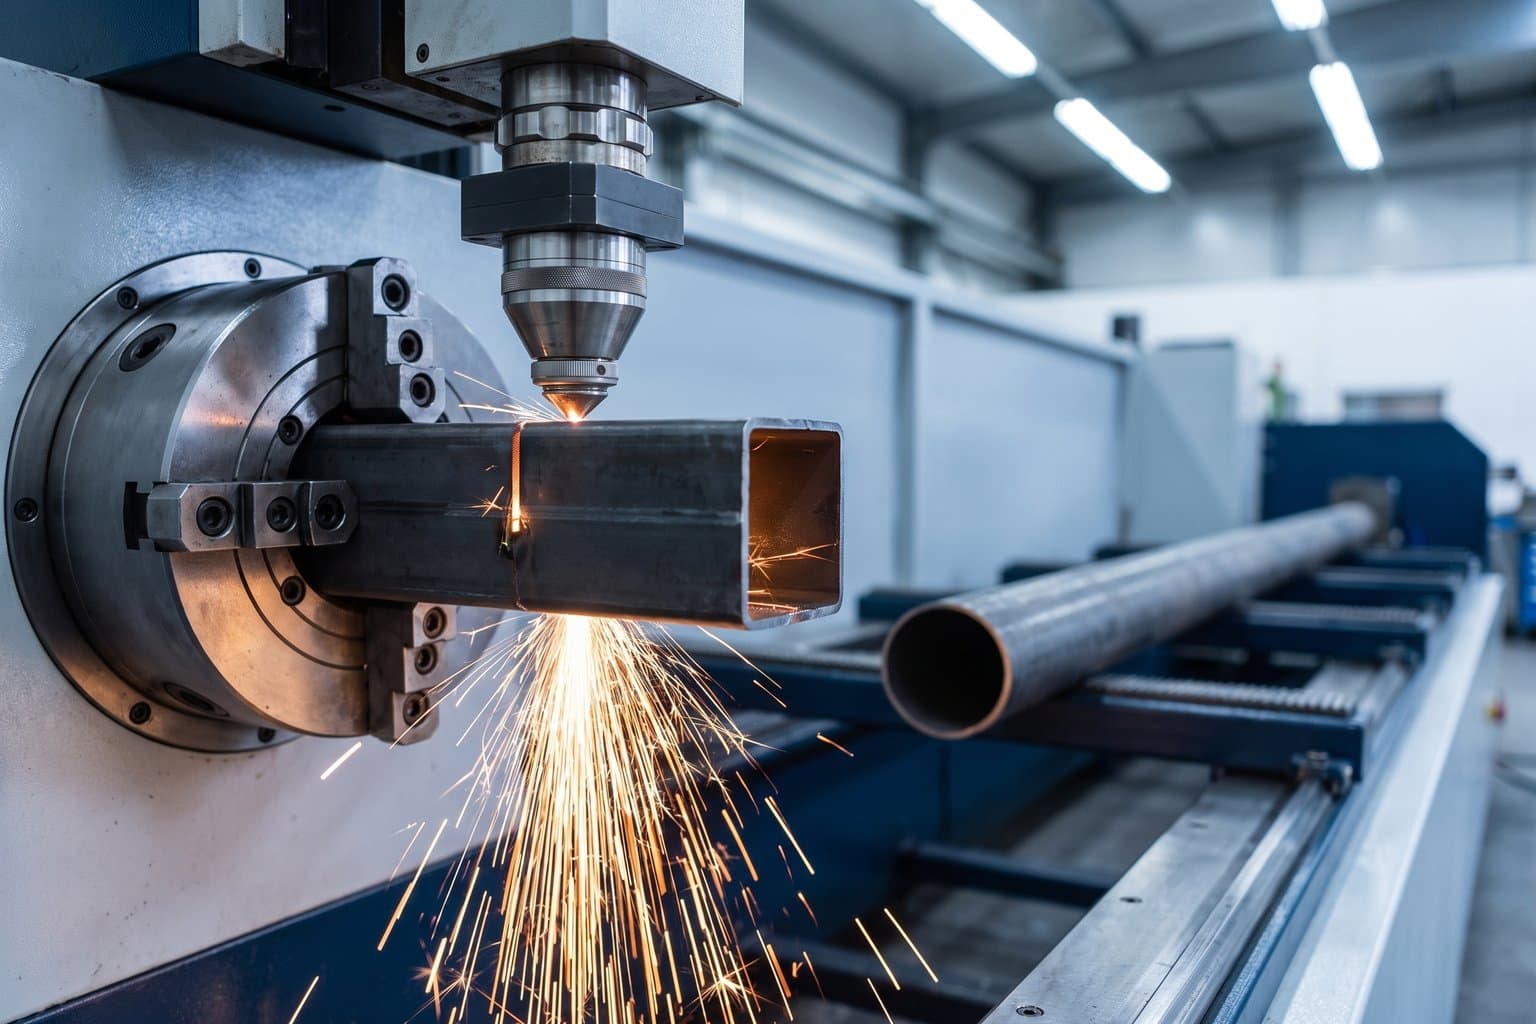
Ask about tube laser capacity and the answer comes back as a diameter. The machines we represent run from about 10 mm to 660 mm round, so somewhere in that range there is one that suits the work.
Diameter is the easy number, and on its own it is close to useless for specifying. Two shops can both say "we run 150 mm round" and need different machines, because the tube one of them buys weighs two and a half times what the other one does.
The constraints that actually decide the machine are weight and stick length. Diameter usually looks after itself.
The capacity ranges we quote against
Four classes of tube laser, described by what they hold rather than by model.
| Class | Round tube | Square tube | Max tube weight | Max stick length |
|---|---|---|---|---|
| Light section | 10 to 120 mm | 10 to 120 mm | 80 kg | 5.0 to 6.5 m |
| Small and medium | 20 to 180 mm | to 180 mm | 260 kg | to 12.2 m |
| General fabrication | 20 to 360 mm | 20 to 350 mm | 300 to 850 kg | 6.2 to 12.2 m |
| Heavy structural | 40 to 660 mm | 40 to 500 mm | 1,200 to 2,500 kg | to 12.0 m |
Profiles are not limited to round and square. Across the tube laser range we quote oval, angle iron, channel and special shaped sections, in carbon steel, stainless, aluminum and copper.
Why does weight decide it, and not diameter?
Weight per metre rises with wall thickness far faster than most buyers expect, and the diameter on the drawing says nothing about it.
Take 150 mm round tube in mild steel. At a 5 mm wall it weighs about 17.9 kg per metre, so a six metre stick is roughly 107 kg. At a 12.5 mm wall the same 150 mm tube weighs about 42.4 kg per metre, and the same six metre stick is roughly 254 kg.
Same diameter on both drawings. One sits comfortably inside a 260 kg chuck rating and the other does not, and no amount of reading the diameter spec tells you that.
This is why the sizing conversation starts with what you buy, not what you cut. Bring the heaviest section you run regularly, in the longest length your supplier delivers, and the class follows from it.
Stick length is the second constraint, and it is a building question
Loading length runs to about 12.2 m at the top of the range. (16m infeed/outfeed lengths are available under special circumstances.) That is enough for mill lengths, and it is where a lot of shops discover the real limit is the building rather than the machine.
A machine that loads 12 m tube needs the floor to feed it and the room to unload it at the other end. Measure the run before the machine, not after. It is a cheaper conversation before an order than after a machine lands in your shop.
What happens to the last piece of every stick?
At the heavy end, the cutting head can cross the centre chuck, which means the last piece of a stick gets cut rather than dropped in the offcut bin. On a shop buying heavy wall structural tube by the tonne, the remnant on every stick is a real material line, not a rounding error.
It is worth asking about specifically. It is a capability that varies across the range and it does not show up in a diameter spec at all.
When is a tube laser the wrong answer?
If the work is a handful of straight cuts a week on common sizes, a saw and a drill are the right tools and a tube laser will sit idle earning nothing. The machine earns its place when the parts carry holes, slots, copes, notches or weld preparation, because that is where it replaces several operations and several handlings rather than one. Shops whose work is mostly flat parts rather than sections are usually better served by sheet and plate laser cutting, and heavy beam work belongs with structural steel processing.
The same caution applies inside the range. A larger machine is not a safer choice. Buy for the sections you actually run, not the largest one you might one day quote, because the capacity you do not use still costs money every shift.
If a Han's machine is not the right answer, we will say so and quote one that is.
What to have ready when you call
Four things, and they settle the class in one conversation:
- The heaviest section you run regularly, with its wall thickness
- The longest stick your supplier actually delivers
- Whether the work is round, square, or includes angle and channel
- The clear floor length available for loading and unloading
We are in Cambridge, Ontario, we stock parts in Canada, and the technicians who commission the machine are the ones who come back to service it. If the answer is that your work does not need a tube laser yet, that is a useful answer too, and we would rather give it before an order than after one.
A note on these figures
These are the published capacities of the tube laser range we represent, taken from our own catalogue. They are the envelope the machines are rated to, not a promise about a specific part. Wall thickness, material grade and the tolerance you need all move what is sensible inside that envelope, which is what the sizing conversation is for.
Weight figures are calculated for mild steel at standard density and are there to show the scale of the difference, not to size a specific order.
About Doug Robinson
Doug leads sales at AC Machinery and takes most of the first calls from buyers specifying cutting equipment. He works with fabricators and steel service centres across Canada, from the first enquiry through to the machine on the floor.
Doug Robinson on LinkedInFAQ
Common questions
Short answers to the questions we are asked most about this topic.
Across the range we represent, up to 660 mm round and 500 mm square, at up to 2,500 kg per stick.
Down to 10 mm round and square on the light section machines.
Both, along with oval and special shaped sections. Angle and channel are common on structural work and are covered at the light section end of the range as well as higher up.
Up to about 12.2 m loading length at the top of the range, which covers standard mill lengths. The practical limit is often the floor space either side of the machine.
Yes, along with copper on part of the range. Material changes the cutting parameters and the sensible thickness, not whether the machine accepts the section.
Start from the heaviest section you buy, in the longest length delivered. Weight per metre and stick length place you in a class faster than diameter does.
Usually not. The return comes from holes, copes, slots and weld preparation done in one handling. Straight cutting alone is a saw's job.